Live monitoring for aluminium extrusion
Press monitoring.For extrusion plants.
OEE, stops and dies, for the people running the press.
- Above target
- On target
- Below target
- Downtime
Click a billet for its press curve.Tap a billet for its press curve.
Press 2 · Shift B
- Availability
- 98.0 %
- Performance
- 94.7 %
- Quality
- 100.0 %
- OEE
- 92.7 %
Ram pressure bar
Ram speed mm/s
Profile temperature °C
- Billet length
- Dead cycle
- Push time
- Paused
- Breakthrough pressure
- End pressure
- Average ram speed
- Peak profile temperature
Customers running Chronos
In production across 33 countries.
Why extruders run Chronos
What the plant gets.
Act now
From operator to maintenance, everyone sees the same figures as they happen.
More on the platformEvery billet traceable
Every signal for every billet stays on record, for a complaint or an audit.
More on reportsNo integration project
Pick the signals off the control system, including the ones that exist only on your machine, and manage them yourself.
More on connecting
Traceability
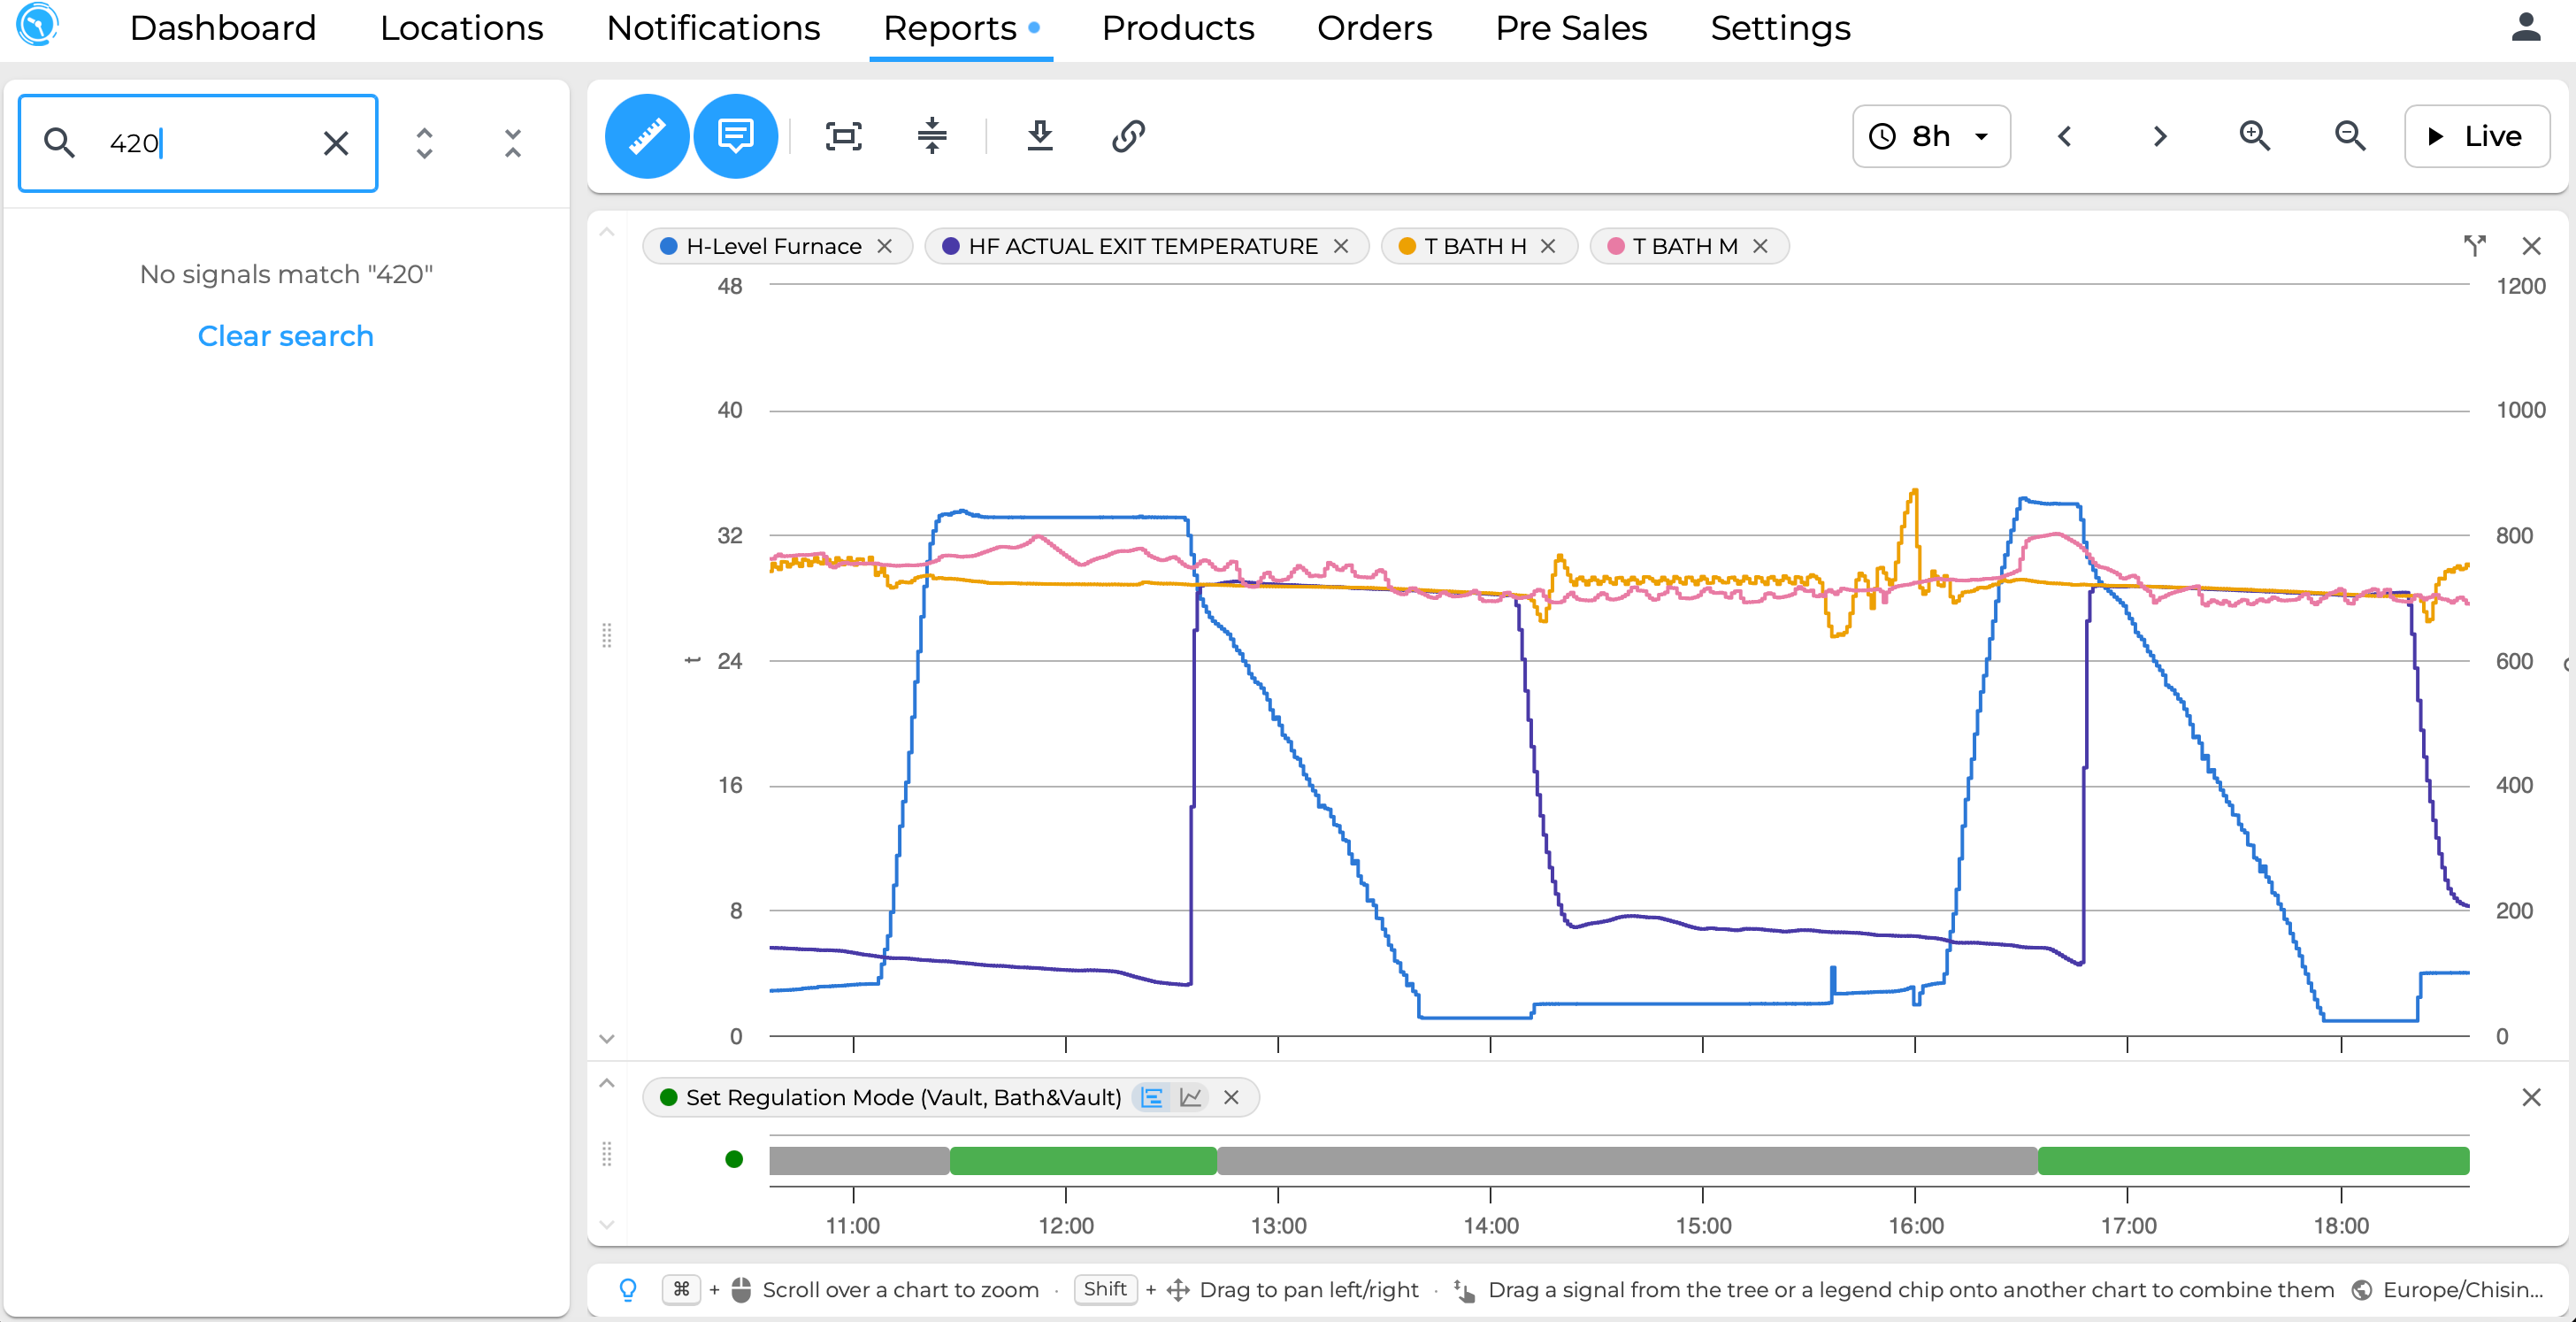
Traceability keeps getting more important, and it is now a requirement: a plant has to record exactly how a product was made. Chronos does that. The signals are stored at full resolution, every 100 ms, for as long as you need them.
Billet 2404:51:14
Order 24-1203Press 2
Ram pressure288 bar
Ram speed10.6 mm/s
Profile temperature588 °C
Billet length1,192 mmPush time104 s
Billet 24, Order 24-1203, Press 2, 04:51:14.Ram pressure 288 bar. Ram speed 10.6 mm/s. Profile temperature 588 °C.Billet length 1,192 mm. Push time 104 s. 122 s.
Optimized for extrusion plants
Detailed press monitoring.
Press quantities
Billet length, butt end, ram-speed ramps, multi-push run-outs and flying cut are part of the press record.
Die life and history
Die life in billets or kilograms, nitriding, die history and OEE per die.
No black-box OEE
Every figure opens into the arithmetic behind it, down to the billet.
Quality in kilograms
Yield from input to output mass, because extrusion is a recovery business.
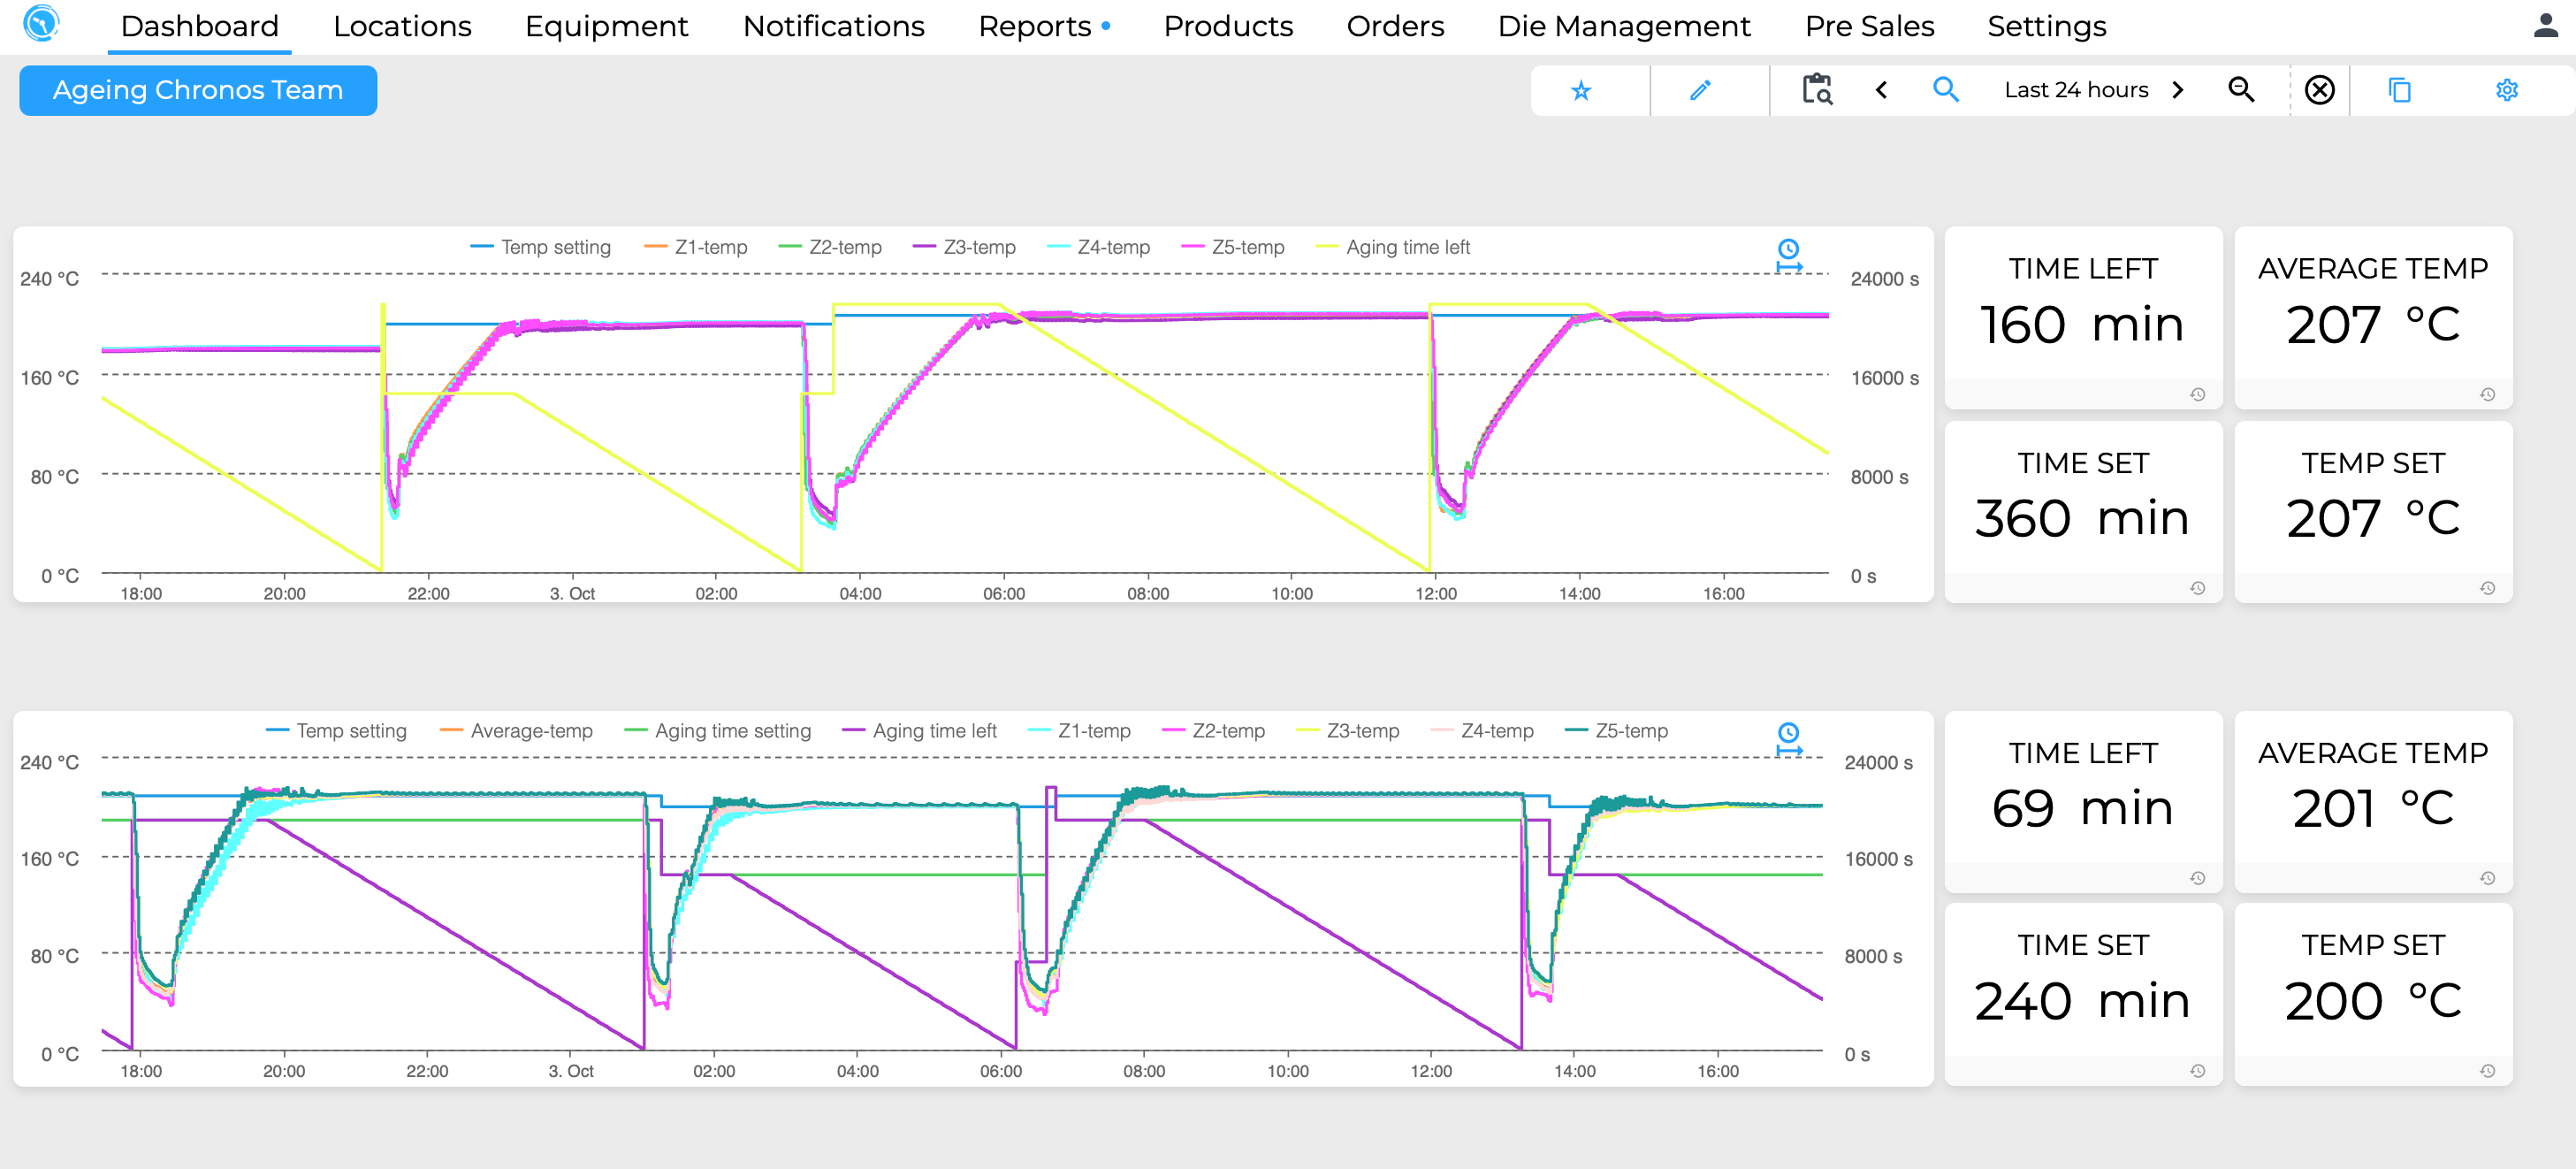
Ageing ovens and casting, too.
The same system records a machine that has no standard. You choose the signals, and Chronos keeps every one of them.
Results
Results from bending, milling and packing.
+30% OEE
Bending machine
In four months, mostly from shorter cycle times.
+27% OEE
Milling robot cell
In two months, once the losses in tool changing were visible.
+80kg / hour
Profile packing
From 450 to 530 kg per hour, once teams could compare how they worked.
Start with one press.
With its PLC on your local network, basic downtime monitoring runs within a few days.